How to Choose the Best Desktop CNC Mill?
Choosing the best desktop CNC mill is not simply a matter of comparing prices, spindle speeds, or attractive photographs. The right machine must match your materials, workspace, projects, skills, and tolerance expectations. A compact mill may cut aluminum cleanly, yet struggle with deeper pockets or long production runs. Another model may offer impressive specifications but lack reliable support, rigid construction, or accessible replacement parts.
John Saunders, founder of NYC CNC and a respected machining educator, captures the learning process clearly: “The best way to learn is to do.” His point matters when evaluating a desktop CNC mill. Hands-on experience reveals details that brochures often hide. Listen for unusual vibration during a test cut. Check whether the worktable feels stable under pressure. Examine the software workflow before committing to complicated hardware. These small observations can prevent expensive frustration.
This guide explores the practical factors behind a confident purchase. It considers machine rigidity, travel range, spindle performance, control software, workholding, safety features, maintenance, and after-sales service. It also examines common mistakes, including choosing maximum specifications over usable performance. That mistake is easy to make.
Your ideal desktop CNC mill may not be the fastest or largest option. It may be the machine that fits your bench, your budget, and your patience. Some compromises are unavoidable. Understanding them is more valuable than chasing perfection. A careful buyer should also accept an uncomfortable truth: no mill can replace sound setup, sharp tooling, and steady operator judgment.
Define Desktop CNC Mills by Axes, Work Envelope, and ISO 230-2 Accuracy
How to Choose the Best Desktop CNC Mill?
A desktop CNC mill should be defined by three measurable features: axes, work envelope, and accuracy. Three-axis machines suit flat plates, brackets, and simple pockets. A fourth rotary axis can expose several faces without repeated clamping. More axes are not automatically better. They also increase programming demands, collision risks, and maintenance points.
Measure the work envelope against the real part, not the advertised maximum. Leave space for clamps, cutters, and chip evacuation. A 300 mm X travel may provide only 220 mm of usable space after fixturing. That detail is easy to miss. ISO 230-2:2014 defines methods for testing positioning accuracy and repeatability, including measurements along each linear axis. It does not give every desktop mill a universal accuracy grade. Therefore, request the machine’s acceptance report.
Look for bidirectional positioning accuracy, repeatability, backlash, and thermal conditions. NIST’s Engineering Statistics Handbook distinguishes repeatability from reproducibility, which matters during long machining cycles. A reported ±0.02 mm result may describe one axis, one temperature, and one test length. It is not a promise for every material. I once treated the smallest catalog tolerance as the machine’s everyday capability. That was too optimistic. Ask for traceable measurement data, test length, probing method, and maintenance history before comparing models. A practical choice often beats a technically impressive one.
Compare Spindle Power, 6,000–24,000 RPM, and ER11/ER16 Tooling
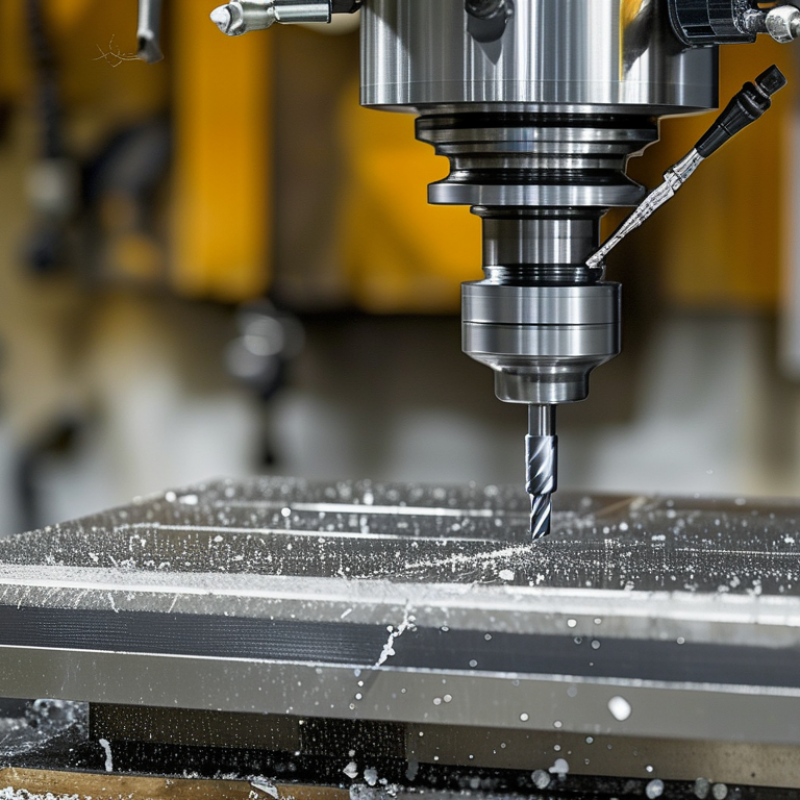
Choosing a desktop CNC mill starts with the spindle, not the advertised maximum speed. In my workshop, a 24,000 RPM spindle handled tiny cutters smoothly, but it struggled when cutting aluminum too aggressively. High speed reduces cutting load on small tools and leaves cleaner edges in wood, plastics, and engraving work. Not always. A 6,000 RPM spindle can deliver stronger low-speed torque for larger cutters and deeper passes. That difference becomes obvious when chips stop flowing and the cutter begins to rub.
Compare spindle power in watts, but read the duty rating and cooling method carefully. A nominal power figure may describe electrical input rather than useful cutting output. Ask whether the spindle maintains speed under load. A practical test is simple: make identical passes in scrap material at two feed rates. Listen for pitch changes, inspect the chips, and check the workpiece temperature. I once trusted a high RPM setting too much. The surface looked polished, yet heat had softened the plastic. That mistake changed my setup more than a specification sheet did.
Tooling matters too. ER11 collets suit smaller shanks and compact cutters, while ER16 accepts a broader range of heavier tooling. Check the included collet sizes; the advertised spindle standard may not include every insert. For fine engraving, ER11 can reduce mass and improve access around tight details. For aluminum or hardwood, ER16 may offer better support, provided the spindle has enough torque. Poor collet cleanliness causes runout, vibration, and uneven tool wear. Measure it carefully with a dial indicator. Even careful buyers can overestimate cutting depth. Leave room for slower feeds.
How to Choose the Best Desktop CNC Mill? - Compare Spindle Power, 6,000–24,000 RPM, and ER11/ER16 Tooling
Note: Actual performance depends on frame rigidity, spindle torque curve, cutter geometry, material, workholding, feed rate, and cutting depth. ER11 and ER16 collets are commonly used with metric and inch tooling within their specified clamping ranges; always verify the spindle and collet manufacturer’s limits before machining.
Match Materials with Rigidity, T-Slot Capacity, and 0.01–0.10 mm Tolerance
How to Choose the Best Desktop CNC Mill?
Choosing a desktop CNC mill starts with the material, not the advertised spindle speed. Aluminum needs a rigid frame, short tool overhang, and controlled cutting forces. Plastics usually tolerate lighter machines, but they can melt when heat builds up. Wood is forgiving, although vibration can leave visible ripples on edges. For steel, many compact mills struggle with rigidity, slow feeds, and tool deflection. I have found that a heavier machine often produces better results than a faster one.
Check the T-slot table before purchasing. Measure its length, width, slot spacing, and usable clamping area. A small table may hold a vise, but leave little room for locating fixtures or repeated setups. T-slot capacity also affects safety. The workpiece must sit flat, with clamps positioned close to the cutting forces. For 0.01–0.10 mm tolerance, inspect the machine after warming up. Check backlash, spindle runout, tool condition, and temperature changes. A 0.01 mm target is demanding. It may be unrealistic on a light frame without careful calibration.
Tips: Use a dial indicator to check movement before precision work. Record offsets and cutting conditions. Measure parts with a calibrated micrometer or suitable gauge. Do not trust one test cut. I once blamed the machine for a poor dimension, then found a loose fixture. That mistake still influences my setup routine. Leave room for doubt. Consistent results matter more than impressive specifications.
How to Choose the Best Desktop CNC Mill?
Typical tolerance ranges for common materials on a properly tuned desktop CNC mill. Lower values require greater machine rigidity, secure T-slot workholding, sharp tooling, and stable cutting conditions.
Aluminum and brass generally demand a more rigid frame and spindle than plastics or hardwood. For heavier workpieces and stronger cutting forces, choose a table with multiple continuous T-slots and robust clamps. A realistic desktop target is approximately 0.01–0.10 mm, depending on material, setup, tool condition, and machine rigidity.
Evaluate Ball Screws, Linear Guides, and Backlash Below 0.05 mm
How to Choose the Best Desktop CNC Mill?
Evaluate Ball Screws, Linear Guides, and Backlash Below 0.05 mm
A desktop CNC mill can look rigid while hiding small mechanical errors. Check the ball screws before judging the enclosure. Ball screws usually provide smoother motion and lower friction than ordinary leadscrews. Inspect the screw support, nut preload, and coupling alignment. Excessive preload can create heat and unnecessary motor load. Too little preload may increase lost motion.
Linear guides deserve equal attention. Move each axis slowly by hand, then feel for tight spots or uneven resistance. Proper guides should maintain smooth travel across the entire stroke. Measure vertical play with a dial indicator near the spindle. A reading above 0.05 mm can affect pockets, fits, and repeated drilling. Keep the indicator mounted firmly.
Backlash is not the same as positioning error. Reverse an axis several times and record the indicator movement. Test near the center and both ends of travel. Temperature matters. A warm screw can expand and change the result. I once measured a promising machine cold, then found noticeably different values after continuous cutting. That mistake changed my testing routine.
Look for repeatable measurements, not impressive specifications alone. Controller compensation may hide backlash during software tests, but it cannot restore mechanical stiffness. Check the machine under light cutting loads. Listen for vibration. Watch the finish. A slightly imperfect test often reveals more than a polished demonstration. Calibration records, maintenance access, and clear adjustment procedures also support reliable long-term accuracy.
Select Controllers, CAM Compatibility, Safety, and Total Ownership Cost
How to Choose the Best Desktop CNC Mill?
Choosing the best desktop CNC mill requires more than comparing spindle speed. The controller determines how confidently you can operate the machine. Check its motion resolution, interface, emergency stop response, and file transfer method. A familiar interface reduces mistakes during setup. Ask whether the controller accepts standard toolpaths from your chosen CAM software. Without reliable compatibility, even excellent mechanical hardware becomes frustrating. My first machine estimate ignored controller updates and replacement cables. That mistake increased downtime and delayed several small projects.
CAM compatibility deserves careful testing before purchase. Confirm supported post processors, axis settings, tool libraries, and work coordinate systems. Run a virtual simulation before cutting material. Then cut a simple test pattern. A reliable workflow should produce matching dimensions repeatedly. Keep notes on feeds, speeds, tool wear, and material changes. If the supplier provides sample files, inspect them instead of trusting promotional claims. Do not trust assumptions.
Safety features should be practical, visible, and easy to maintain. Look for an enclosure, interlocked access, effective chip control, and a clearly reachable emergency stop. Place the mill on a rigid surface with enough space for inspection and cleaning. Noise, dust, and sharp chips affect comfort and long-term use. Total ownership cost includes tooling, collets, software, maintenance, electricity, training, and wasted material. Calculate these costs over three years, not one weekend. I would also reserve money for unexpected repairs. Budgeting is never perfect. Leave room for learning.