7 Best RTO Manufacturers for Global Buyers?
Choosing the right RTO manufacturer can shape emission performance, operating costs, and production reliability for years. This decision deserves more than a polished brochure or an impressive efficiency figure. Global buyers must examine combustion stability, heat recovery, pressure drop, controls, maintenance access, and local service capability. A technically strong RTO can still disappoint if spare parts arrive slowly or commissioning support remains weak.
Dr. Richard C. Flagan, an internationally recognized air-pollution-control researcher, has emphasized, “Control technology must be evaluated as part of the entire process, not in isolation.” That principle guides this review. An RTO should match the process chemistry, solvent loading, airflow variation, and required destruction efficiency. Stainless-steel details matter. So do valve design, refractory quality, burner response, and documented field results. Small omissions can become expensive shutdowns.
This guide examines seven leading RTO manufacturers serving international buyers. The comparison considers engineering depth, customization, energy performance, compliance support, installation experience, and after-sales service. It also considers evidence, not marketing language. Manufacturer reputation varies by region, application, and project scale. No ranking is perfect. A supplier that suits a coating plant may not suit a chemical facility with corrosive exhaust. Buyers should challenge every claim, request comparable references, and verify lifecycle assumptions before signing. Real performance begins with honest data. Sometimes, the cheapest quotation becomes the costliest decision.
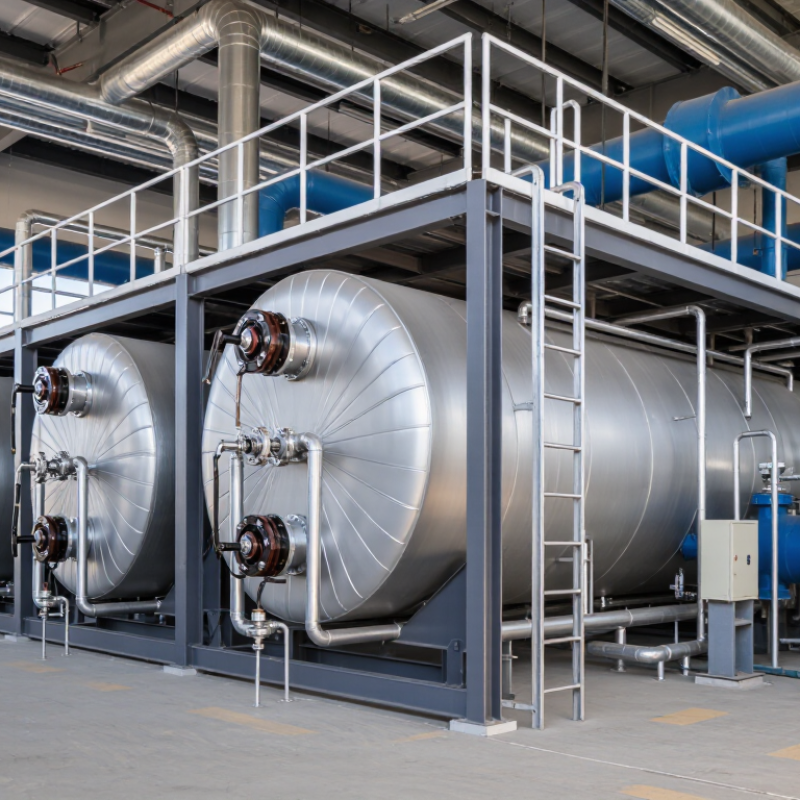
What Is a Regenerative Thermal Oxidizer and How Does It Work?
A regenerative thermal oxidizer, or RTO, controls volatile organic compounds from industrial exhaust. It uses high heat to convert pollutants into carbon dioxide and water vapor. The process is straightforward, but the engineering is not. Gas enters a ceramic heat-storage bed, where recovered heat raises its temperature. A combustion chamber then provides the extra energy needed for oxidation.
After treatment, the hot, cleaner gas passes through another ceramic bed. This bed absorbs heat before the gas leaves the system. Directional valves then reverse the airflow, allowing the stored heat to warm incoming exhaust. It is a repeating cycle. The system can achieve strong heat recovery, often reducing fuel demand compared with a conventional thermal oxidizer. In practice, performance depends on residence time, operating temperature, mixing, and stable airflow.
A buyer should examine valve durability, ceramic media quality, pressure drop, and control-system response. A small pressure change can affect fans and production equipment. Regular inspections should check bed fouling, leaks, burner condition, and temperature sensors. High moisture or sticky compounds may require pretreatment. Do not assume every RTO suits every process. That assumption causes trouble. Site tests, emission data, and maintenance records provide more reliable evidence than catalog ratings. Even a well-designed unit may underperform when exhaust volume changes sharply during shift operations.
What Is a Regenerative Thermal Oxidizer and How Does It Work?
Typical performance ranges below are commonly used for preliminary RTO selection. Actual results depend on VOC composition, inlet concentration, airflow, operating temperature, residence time, and system design.
RTOs destroy VOCs by heating contaminated process air in a combustion chamber. Ceramic heat-storage media recover thermal energy from the treated exhaust and transfer it to the incoming air, reducing fuel consumption. Typical VOC destruction efficiency is approximately 95–99%, while thermal recovery is commonly around 85–95%.
Reference: U.S. EPA, Air Pollution Control Technology Fact Sheet—Regenerative Incinerators.
Seven Leading RTO Manufacturers for International Buyers
Seven Leading RTO Manufacturers for International Buyers
International buyers often compare seven manufacturer profiles: engineered-to-order specialists, modular system suppliers, low-flow experts, high-temperature process designers, solvent-recovery integrators, aftermarket service providers, and regional fabricators. The strongest suppliers document residence time, chamber temperature, pressure drop, and guaranteed VOC destruction efficiency. The U.S. EPA Air Pollution Control Cost Manual reports that well-designed regenerative thermal oxidizers can achieve destruction efficiencies near 95–99%. However, field results depend on airflow variation, contaminants, maintenance, and commissioning quality.
Market data supports continued investment. The MarketsandMarkets Air Pollution Control Systems report projects steady global growth through 2028, driven by stricter industrial emissions controls and expanding manufacturing capacity. For overseas projects, a capable manufacturer should provide CE or equivalent compliance support, corrosion-resistant materials, remote diagnostics, and spare-part planning. Experience matters here. A low purchase price can become expensive when burners, ceramic media, or control components are unavailable locally. One weakness remains: published efficiency figures often reflect stable test conditions, not every factory shift.
Tips: Ask each of the seven shortlisted manufacturers for three comparable references, certified test results, energy consumption at your actual flow rate, and a written warranty. Request a failure-response timetable. Small details matter. Check whether manuals, alarms, and operator training are available in your working language. EPA guidance and ISO 14001 practices can strengthen supplier evaluation, but they do not replace an independent performance test.
Comparing RTO Technologies, Industries, and Service Capabilities
7 Best RTO Manufacturers for Global Buyers?
Choosing among the seven best RTO manufacturers requires more than comparing catalog prices. Regenerative thermal oxidizers differ in bed design, valve layout, heat recovery, and control logic. Three-bed systems can support steady VOC loads, while rotary designs may reduce valve movement and maintenance points. Ceramic media also matters. Dense structured media can improve heat transfer, but it may cost more and require careful cleaning.
Industry conditions shape the right choice. Chemical plants often need corrosion-resistant materials and flexible operating ranges. Coating lines may demand quick response to changing solvent loads. Pharmaceutical facilities usually require documented validation and stable temperature control. Food processing sites may face humidity, odors, and sticky contaminants. In plant evaluations, I check gas flow, VOC concentration, moisture, dust, and available floor space before reviewing proposals.
Service capability is equally important. Strong manufacturers provide process calculations, emission estimates, detailed drawings, factory testing, and on-site commissioning. They should train operators beside the control panel, not only send a manual. Spare valve seals, thermocouples, and ceramic media should have clear delivery times. Remote diagnostics can reduce downtime, but it cannot replace local technicians. A polished proposal can still hide weak after-sales support. I have seen projects underestimate duct modifications, access platforms, and future maintenance space. That mistake becomes expensive. Ask for references from similar industries, verified performance data, warranty limits, and a realistic service plan.
How to Choose the Best RTO Supplier for Your Project
RTO selection starts with emission facts, not brochure claims. Measure VOC type, concentration, flow variation, moisture, particulates, and operating hours. An RTO sized for peak flow may waste fuel at normal load. An undersized unit creates pressure, maintenance, and compliance risks. Keep the data honest.
The U.S. EPA’s Air Pollution Control Technology Fact Sheet reports typical RTO VOC destruction efficiencies of 95–99%. It also reports thermal energy recovery commonly reaching 85–97%. Treat these figures as reference ranges, not guarantees. Ask each supplier for tested performance at your actual inlet conditions. Request evidence for solvent mixtures, low-load operation, startup, and bypass events. A useful proposal should show pressure drop, fuel use, chamber temperature, residence time, and expected uptime. Numbers matter.
Inspect the engineering behind those numbers. Compare valve design, refractory construction, heat-recovery layout, controls, sensor redundancy, and cleaning access. The European Commission’s Industrial Emissions BREF emphasizes monitoring, stable combustion, and energy efficiency in thermal treatment systems. Ask how alarms are recorded and calibration is managed. Speak with operators running similar processes. Short visits reveal more than polished presentations. Check service response times, spare-part availability, commissioning support, and training. A low purchase price can become expensive through fuel, downtime, or difficult maintenance. No scorecard is perfect. Weight risks openly, and document assumptions before signing.
7 Best RTO Manufacturers for Global Buyers? - How to Choose the Best RTO Supplier for Your Project
| Evaluation Profile | Typical RTO Configuration | Typical VOC Destruction Efficiency | Heat Recovery Range | Typical Operating Temperature | Best Application Fit | Key Supplier Capability to Verify |
| Profile 1: High-Efficiency Three-Bed System | Three-bed regenerative thermal oxidizer with ceramic heat-storage media | Up to approximately 99% | 90%–97% | 760–980°C | Continuous VOC emissions with relatively stable airflow | Valve durability, switching-cycle control, ceramic-media quality, and guaranteed outlet emissions |
| Profile 2: Low-Concentration VOC Specialist | Direct-fired or regenerative system with supplemental natural-gas support | 95%–99% | 85%–95% | 760–950°C | Large exhaust volumes with low or fluctuating VOC loading | Fuel-consumption calculations, minimum operating concentration, and low-load stability |
| Profile 3: High-Flow Industrial Supplier | Modular two- or three-chamber RTO designed for high volumetric flow | 95%–99% | 90%–96% | 800–1,000°C | Coating, printing, chemical, and process lines with large airflow | Pressure-drop data, fan sizing, expansion allowance, and modular installation planning |
| Profile 4: High-Humidity and Condensable VOC Specialist | RTO with preconditioning, condensate management, and accessible media sections | 95%–99% | 85%–95% | 760–980°C | Processes containing moisture, aerosols, heavy hydrocarbons, or sticky compounds | Condensation control, fouling prevention, drain design, and media-cleaning procedures |
| Profile 5: Variable-Flow Process Integrator | RTO with variable-frequency drives, bypass control, and automated flow balancing | 95%–99% | 88%–96% | 760–980°C | Batch production, multiple production lines, and frequently changing exhaust volumes | Turndown performance, control logic, response time, and integration with plant automation |
| Profile 6: Heat-Recovery-Oriented Supplier | RTO with secondary heat exchanger for hot water, thermal oil, or process-air recovery | 95%–99% | 90%–97% plus secondary recovery | 800–1,000°C | Facilities that can continuously use recovered thermal energy | Energy balance, heat-exchanger fouling risk, recovered-energy guarantees, and utility interfaces |
| Profile 7: Export and Lifecycle-Service Specialist | Standardized RTO package with remote monitoring, spare parts, and commissioning support | 95%–99% | 90%–96% | 760–980°C | International projects requiring documentation, training, and long-term maintenance | Applicable standards, local service coverage, spare-parts lead time, FAT/SAT procedures, and warranty terms |
Buyer’s note: The performance figures above are typical industry design ranges rather than rankings of named companies. Actual results depend on VOC chemistry, inlet concentration, airflow, moisture, residence time, operating temperature, permitted limits, and test methods. Request a project-specific mass and energy balance, guaranteed outlet-emission values, pressure-drop data, fuel-consumption figures, and acceptance-test criteria before selecting a supplier.